apbclothing
  • Home
  • Featured
  • Hair Style
  • Makeup
  • Skincare
Category:

Machine

Machine

How Machine Learning Algorithms Modernize Revenue Assurance in Telecom Operations

by apbclothing November 10, 2026
written by apbclothing

Telecom operators process enormous volumes of customer, network, charging, and payment data every day. Even small inconsistencies between these records can result in missed charges, incorrect invoices, or unexplained settlement differences. Traditional audits often detect such problems only after financial discrepancies have accumulated.


Applying machine learning to revenue assurance in telecom enables operators to identify unusual patterns earlier, investigate potential losses more efficiently, and build a clearer picture of how service activity translates into revenue. Whale Cloud’s digital transformation expertise reflects the broader industry shift toward connecting operational data with more intelligent business processes.


Detecting Revenue Leakage Through Pattern Recognition

Revenue leakage rarely comes from a single source. Missing usage records, outdated tariff configurations, duplicated transactions, and incorrect discount rules can each create discrepancies between delivered services and billed amounts. Conventional checks are effective at identifying predefined errors, but unfamiliar patterns may remain unnoticed until an analyst investigates them manually.


Machine learning offers another layer of detection by learning from historical transaction data. Anomaly detection models can identify deviations in call volumes, charging amounts, settlement values, or customer activity. For example, a sudden drop in billable usage records may indicate a mediation problem rather than a genuine decline in demand. The model highlights the deviation, while operational teams investigate its cause.


Effective revenue assurance in telecom requires more than flagging unusual transactions. Alerts need to be ranked according to financial exposure, recurrence, and operational urgency. A minor discrepancy affecting one low-value transaction may require less attention than a recurring configuration error across thousands of accounts. Prioritization helps analysts concentrate on issues with the greatest potential business impact.


Connecting Data Across Billing and Business Support Systems

Reliable analysis depends on consistent data from multiple platforms. Network systems record service usage, mediation platforms process event records, charging engines calculate fees, and billing applications generate customer invoices. Differences in timestamps, identifiers, and data formats can prevent these records from being matched accurately, limiting the usefulness of even sophisticated algorithms.


A well-integrated BSS system can provide an important foundation for connecting customer, product, charging, and billing information. Machine learning models can then analyze relationships across these records to identify missing transactions, inconsistent charges, and unusual changes in customer behavior. Data validation remains essential because incomplete or incorrectly labeled records can produce misleading findings.


Customer-level analysis adds another dimension. A unified customer view can connect subscription details, service usage, account adjustments, payment history, and relevant interaction records. This context helps distinguish legitimate billing variations from suspicious anomalies. Operators should apply appropriate access controls and data minimization practices, particularly when customer information is shared across analytics environments.


Improving Risk Assessment With Predictive Analytics

Historical discrepancies can help models estimate where future problems are more likely to occur. Repeated failures following tariff updates, product launches, or system migrations may reveal control weaknesses that deserve additional scrutiny. Predictive models can assign risk scores to transaction groups, helping teams schedule audits before issues affect a large number of accounts.


Model performance depends on the quality and representativeness of training data. Telecom services change frequently, and a pattern that once indicated fraud or a billing defect may become normal after a commercial policy update. Regular retraining, drift monitoring, and feedback from investigators help maintain relevance as operating conditions evolve. Human review remains important, particularly when model findings could trigger financial adjustments or customer disputes.


Machine learning also supports root-cause analysis by grouping similar exceptions across systems and time periods. If multiple discrepancies share a common product configuration or interface, the underlying problem may lie in a system change rather than individual transactions. This approach moves revenue assurance in telecom beyond case-by-case correction toward identifying recurring process weaknesses and preventing their return.


Applying Intelligent Analytics to Operational Decisions

Technology becomes useful when its findings connect directly to established workflows. An alert should include the affected records, the likely discrepancy category, supporting evidence, and a clear route for investigation. Integration with case-management tools allows analysts to record decisions, assign responsibilities, and track whether corrective actions resolve the underlying problem.


Whale Cloud describes a smart 360-degree customer-view capability designed to extract and connect customer data from dozens of previously isolated systems for a Southeast Asian telecom operator. This example illustrates how unified information can support broader analytics and operational decision-making. Its relevance to financial controls depends on the available data, integration scope, and specific revenue-assurance functions implemented.


Operators can evaluate results through measurable indicators such as the value of validated leakage, the time required to resolve exceptions, false-positive rates, and the recurrence of known issues. A BSS system integrated with analytical tools can help connect billing operations with these measurements, provided that source records remain traceable and control ownership is clearly defined. Performance reviews should distinguish confirmed financial recovery from estimated exposure to avoid overstating benefits.


Conclusion

Machine learning changes financial control from a process based mainly on retrospective checks into one that can detect patterns, assess risks, and guide earlier investigations. Reliable results still depend on sound data integration, transparent decision rules, and experienced staff who can validate unusual findings before corrective action is taken. Applied thoughtfully, revenue assurance in telecom can become a more continuous and evidence-based operational discipline.


Whale Cloud‘s focus on connected customer data offers a relevant reference for operators seeking to improve visibility across fragmented systems. When analytical capabilities work alongside a well-integrated BSS system, telecom businesses can investigate discrepancies with greater context, prioritize financial risks, and address the process weaknesses behind recurring losses.
 

November 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

Why Are Aerospace Companies Adopting a Handheld Laser 3D Scanner?

by apbclothing November 10, 2026
written by apbclothing

Aerospace manufacturing demands rigorous dimensional control, repeatable inspection, and reliable documentation across complex components. From turbine parts and structural panels to assemblies requiring precise alignment, even small geometric deviations can create expensive production or maintenance challenges. Traditional inspection methods remain essential, but they may require considerable setup or struggle to capture intricate surfaces efficiently. Portable optical metrology is gaining attention because it brings detailed three-dimensional measurement closer to the component, helping aerospace teams improve inspection workflows and make informed quality decisions.


Inspecting Complex Aerospace Geometries More Efficiently


Aircraft components often feature curved surfaces, narrow grooves, intricate contours, and multiple interconnected features. Measuring these details with conventional tools can require numerous individual readings and repeated repositioning. Such procedures may extend inspection cycles, particularly when engineers need to assess an entire surface rather than a few predefined dimensions.


A handheld 3D scanner captures dense three-dimensional data across accessible surfaces, creating a digital representation of the physical component. Engineers can compare this data with the original CAD model to identify deviations and investigate potential manufacturing issues. This approach is especially useful for complex geometries where broader surface coverage provides more insight than isolated measurements.


Bringing Measurement Directly to the Workpiece


Moving large aerospace components between production areas and dedicated metrology laboratories can consume valuable time. Some structures are also difficult to position securely because of their size, weight, or assembly status. Portable scanning reduces dependence on transporting every component to a fixed measurement station.


A handheld laser 3D scanner can be operated near the production line, in an inspection area, or in a suitable maintenance facility. Engineers can collect dimensional data where the work occurs, helping teams investigate fit issues and manufacturing deviations sooner. The practical benefit depends on access, environmental conditions, required accuracy, and the availability of appropriate reference data.


Supporting Quality Control and Earlier Defect Detection


Aerospace quality teams must identify dimensional deviations before they affect subsequent manufacturing or assembly operations. Problems involving surface profiles, hole locations, alignment, or component deformation can lead to additional machining, repeated inspections, or costly part rejection if discovered late.


Three-dimensional scanning provides a broader dataset for evaluating component geometry. When scan data is aligned with nominal design information, color deviation maps and dimensional reports can help engineers locate areas requiring further investigation. This supports first-article inspection, production verification, and selected maintenance tasks, although acceptance decisions must still follow applicable engineering requirements and approved inspection procedures.


Improving Productivity Across Inspection Workflows


Inspection efficiency involves more than the speed of data acquisition. Equipment setup, operator handling, surface preparation, data processing, and report generation all contribute to the overall cycle time. A practical scanning solution should help reduce unnecessary steps without compromising measurement reliability.


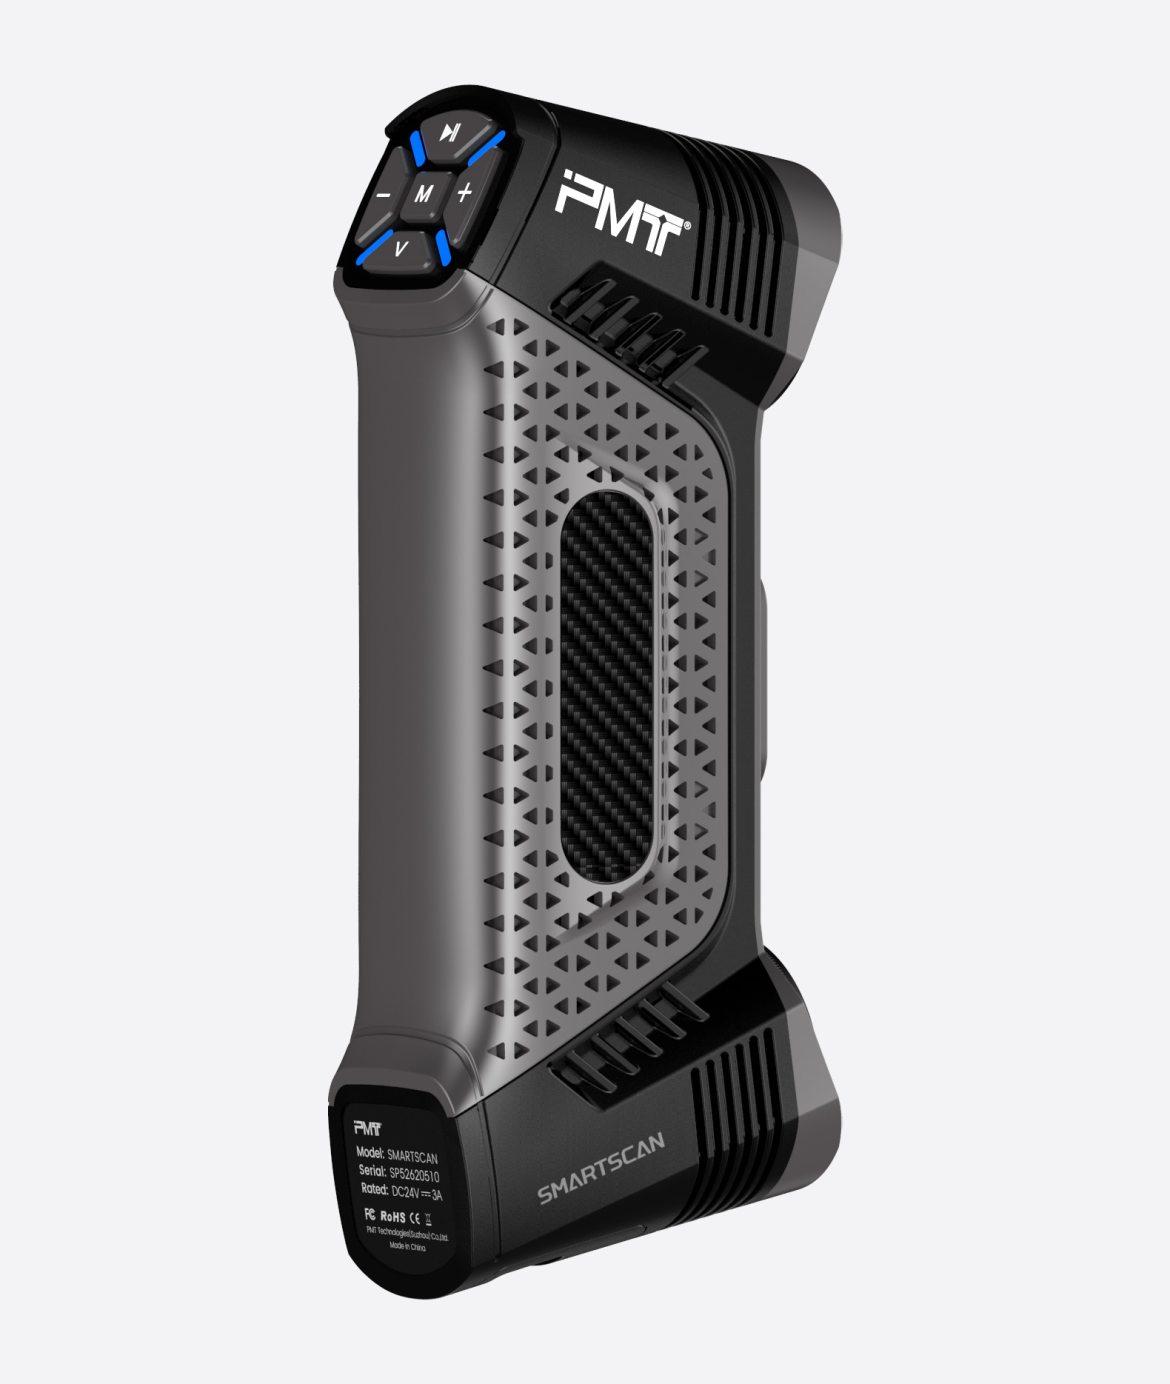
PMT’s SMARTSCAN handheld laser 3D scanner offers a portable, non-contact measurement approach designed to capture workpiece details on-site. The device weighs approximately 530 grams, excluding the battery, and supports a maximum field of view of 700 × 600 mm. These characteristics can help operators handle scanning tasks across different work areas while collecting detailed surface information.


The handheld 3D scanner also supports integration with SkyForm scanning software and PMT INSPECT 3D measurement software for dimensional analysis. Such workflows can help teams move from data capture to CAD comparison and reporting more efficiently, depending on the inspection task and software configuration.


Addressing Maintenance, Repair, and Component Verification


Aerospace maintenance, repair, and overhaul operations often involve assessing used components whose geometry may have changed through wear, impact, or repeated service. Reliable dimensional information helps technicians determine whether a component requires closer examination or additional engineering evaluation.


Portable scanning can document surface conditions and support comparisons between current measurements and reference geometry. Repeated scans may also help teams monitor dimensional changes over time, provided measurement procedures remain consistent. However, optical scanning does not automatically replace nondestructive testing, internal defect detection, or other inspections required to establish component serviceability.


Choosing Equipment Based on Aerospace Requirements


Adopting a scanning system requires more than comparing advertised accuracy figures. Aerospace buyers should evaluate measurement uncertainty, repeatability, traceability, software compatibility, surface characteristics, and the dimensions of typical components. Calibration and validation procedures must demonstrate that the equipment is suitable for each intended application.


PMT’s SMARTSCAN handheld 3D scanner is designed for industrial measurement tasks and offers multiple scanning modes for different geometric requirements. Its lightweight construction and on-site operation may suit manufacturers seeking more flexible dimensional inspection. Before deployment, quality teams should validate the complete measurement process against applicable tolerances and customer or regulatory requirements.


A controlled pilot project can provide a realistic basis for investment decisions. Comparing inspection duration, defect detection, operator workload, and reporting effort against the existing process helps quantify benefits without assuming every component will deliver the same productivity gains.


Building a More Flexible Aerospace Inspection Strategy


Aerospace companies are adopting portable three-dimensional metrology to address complex geometry, reduce unnecessary component handling, and obtain useful dimensional information closer to production and maintenance activities. The greatest benefits arise when scanning complements established quality procedures rather than replacing necessary verification methods.


For manufacturers evaluating a handheld laser 3D scanner, PMT’s SMARTSCAN provides a lightweight, non-contact option for capturing detailed component geometry and supporting digital inspection workflows. With appropriate validation, software integration, and operator training, this technology can help aerospace teams improve measurement efficiency while maintaining the accuracy, documentation, and quality controls their operations require.


November 10, 2026 0 comments
0 FacebookTwitterPinterestEmail
IndustryMachine

Custom Resistance Welding Manufacturer vs. Standard Machine Suppliers: Which Is Better for Battery Packs?

by apbclothing October 14, 2026
written by apbclothing

Battery-pack welding is rarely a case of simply choosing a machine with enough welding current. Cell format, busbar geometry, material combinations, joint location, electrode access, production volume, and inspection requirements can all affect the equipment architecture.


That makes the choice between a custom resistance welding manufacturer and a standard machine supplier a process-engineering decision, not merely a purchasing comparison.


For battery manufacturers, the central question is more practical: does the product fit an established machine platform, or does the welding process itself need to be developed around the product?


The Machine Should Follow the Battery Design


Battery-pack construction can involve numerous conductive joints, including cell-to-tab and busbar connections. The U.S. Department of Energy identifies resistance spot welding as one of the joining technologies used for battery cell manufacturing and specifically highlights welding current, welding time, and electrode force as parameters requiring real-time attention.


That matters because a standardized machine starts with an existing mechanical and control architecture. If the pack design already matches the machine’s electrode approach, workpiece dimensions, tooling arrangement, and process window, standardization can reduce engineering effort.


A different situation emerges when the joint is difficult to access, materials differ from conventional applications, or the welding sequence must coordinate with an unusual assembly process. Here, the equipment needs to adapt to the product rather than forcing the product into a predetermined machine configuration.


Standard Equipment Works When the Process Is Already Known


Standard machinery has a legitimate role in battery production. A proven platform can shorten equipment selection, simplify operator training, and make replacement components easier to standardize across a factory.


Its strongest economic case appears when the manufacturer has a stable product family, repeatable joint geometry, predictable production volume, and a welding process that has already been validated. Under those conditions, paying for extensive customization may add engineering work without creating proportional manufacturing value.


The risk is assuming that a standard machine remains suitable after the battery design changes. A new cell arrangement or busbar geometry can alter electrode access, clamping requirements, weld schedules, and handling. What looked inexpensive at procurement can become expensive during integration if modifications are required after delivery.


Customization Matters Most at the Process-Development Stage


Customization becomes more meaningful when welding is still being developed. Battery manufacturers may need to determine an appropriate combination of current, time, force, electrode configuration, and material stack before freezing the production process. The DOE’s battery-manufacturing research specifically identifies real-time monitoring and feedback as important areas for improving joining performance.


A resistance welding manufacturer involved early in this stage can potentially design the machine around the validated process rather than retrofit an existing platform afterward. The value is therefore not simply a different fixture or electrode. It can involve coordinated mechanical tooling, welding control, sensing, data acquisition, and automation interfaces.


For engineering teams launching a new battery pack, that distinction can affect development time. Equipment that accommodates process trials and subsequent production requirements may reduce the gap between laboratory validation and factory deployment.


Quality Data Separates a Machine Purchase From a Manufacturing System


Battery welding also changes the meaning of “machine quality.” A machine that produces a weld is only one part of the manufacturing system. Engineers increasingly need evidence that the joining process remains inside its defined operating window during production.


DOE research on battery joining identifies real-time monitoring of parameters and joint quality as a development priority. For resistance spot welding, the referenced parameters include welding time, current, and electrode force, while quality objectives can include characteristics such as weld nugget size and joint condition.


A customized resistance welding solutions package can therefore be evaluated by how effectively its controls and data architecture support process validation, alarms, parameter management, and production records. Standard equipment may already provide suitable functions, but the critical question is whether those functions match the manufacturer’s actual quality strategy.


Research from the U.S. DRIVE program also demonstrates the direction of development: inline signals can be analyzed to identify deviations in resistance spot-welding quality and support automated quality decisions.


Compare the Change Cost, Not Just the Machine Price


The cheapest quotation is not necessarily the lowest-cost manufacturing option. Procurement teams should calculate what happens after the machine enters production.


A standard machine may have a lower initial engineering burden, but additional tooling, external automation, software modification, or integration work can increase the total project cost. A customized system may require more engineering at the beginning while reducing adaptation work during commissioning.


The comparison should therefore include process-development support, fixture changes, controls integration, spare parts, maintenance access, programming, commissioning, and future product revisions. Production downtime also deserves attention because a machine that is difficult to modify can become a constraint when the battery design evolves.


This is particularly relevant to facilities developing multiple pack configurations. The U.S. Department of Energy has emphasized flexible, scalable, and highly controllable manufacturing platforms as part of broader battery-manufacturing development efforts.


What a Battery Manufacturer Should Ask Before Signing the PO


The first question for any supplier should be whether the proposed equipment can reproduce the required weld process under actual production conditions. Engineers should provide material combinations, thicknesses, joint geometry, expected takt, electrode access, cooling requirements, automation interfaces, and quality-monitoring objectives.


A capable resistance welding manufacturer should then explain which elements are standard and which require engineering changes. That distinction makes quotations easier to compare and exposes hidden integration work before the purchase order is released.


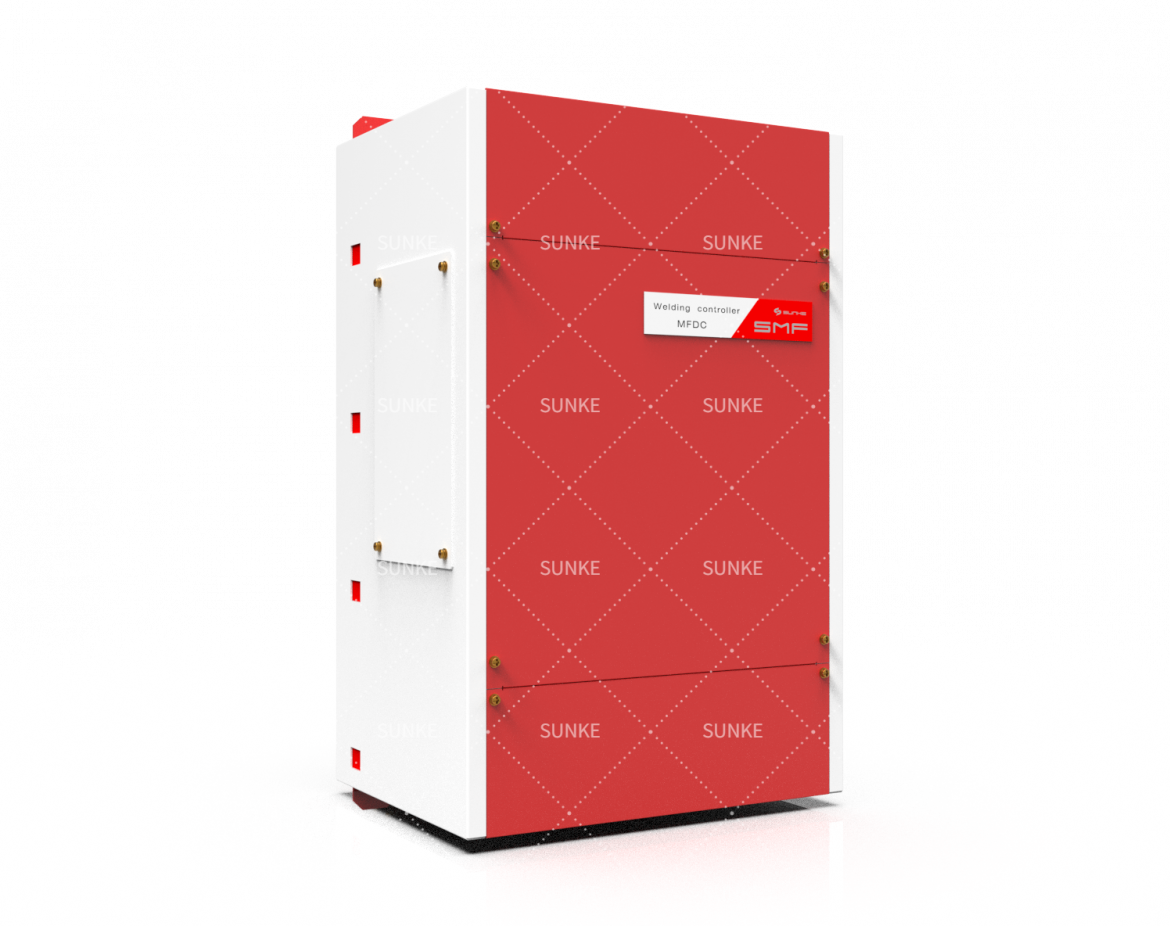
Sunke can be considered when the project requires the welding controller and process architecture to be evaluated together rather than treating the welding power source as an isolated component. Its position in the resistance-welding equipment field makes the distinction between standardized hardware and application-specific engineering relevant to battery manufacturers evaluating new production lines.


For procurement teams, resistance welding solutions should ultimately be judged against the battery’s manufacturing requirements, not against a generic machine specification sheet. A standard machine is appropriate when the product and process already fit the platform. Custom engineering becomes more compelling when joint geometry, process development, quality monitoring, or automation integration creates requirements outside that platform.


Sunke‘s role can therefore be assessed on the same practical basis as any specialist supplier: how well its equipment architecture addresses the defined process, how clearly the supplier identifies customization boundaries, and whether the resulting system can support production rather than merely pass an equipment acceptance test.


The better choice is consequently determined by process maturity. Mature, repeatable battery-pack welding can benefit from standardization. New or highly specific joining processes may justify customization because engineering flexibility has direct value during development and scale-up. The purchasing decision should reflect that difference instead of assuming that either custom equipment or standard equipment is universally superior.


October 14, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

Navigating Supply Chain Risks When Sourcing Light Pink Poly Mailers for Modern E-Commerce Brands

by apbclothing October 12, 2026
written by apbclothing

In today’s competitive e-commerce landscape, unboxing experiences hold significant marketing value. Retailers increasingly lean toward aesthetic shipping supplies to captivate consumers right on their doorstep. As social media sharing and user-generated content continue to drive brand exposure, beautifully designed packaging has become a low-cost yet high-impact marketing tool for online stores.


Among these choices, aesthetic packaging has surged in popularity, making custom hues vital for brand differentiation. However, scaling up the procurement of such customized packaging introduces unique supply chain vulnerabilities.


B2B procurement managers often encounter hurdles ranging from color consistency issues to material scarcity. Understanding these bottlenecks is critical for maintaining seamless logistics and safeguarding brand reputation in the long run.


Identifying Key Vulnerabilities in Specialized Packaging Procurement


Procuring customized mailing supplies is vastly different from buying standard, clear, or monochrome shipping bags. When brands introduce specific branding elements—such as pastel shades—the complexity of the supply chain increases exponentially. Unlike ordinary neutral packaging that allows minor visual errors, soft tones like light pink are extremely sensitive to subtle production deviations, making quality standardization far more challenging for ordinary factories.


One major vulnerability involves pigment consistency and batch variation. Achieving an exact hue across thousands of production runs requires strict mastery over masterbatch mixing and extrusion temperatures. Every tiny change in heating temperature, mixing duration, or pigment proportion can lead to visible color deviation in the finished products. If a manufacturer relies on outsourced raw materials, slight variances can lead to noticeable shade differences between shipments.


For businesses relying on a distinct visual identity, inconsistent deliveries can disrupt brand uniformity, confuse loyal customers, and weaken the premium positioning of high-end beauty and fashion brands.


Additionally, lead time volatility often plagues traditional supply chains. Many intermediaries and trading companies do not control the manufacturing process directly. They can only pass on order demands to upstream factories without the ability to supervise production progress or adjust schedules flexibly. When global resin markets fluctuate or logistics bottlenecks occur, these middlemen struggle to guarantee timely fulfillment. B2B enterprises that fail to partner with direct-source manufacturers frequently face sudden stockouts, delayed order dispatch, and inflated purchasing costs during peak shopping seasons such as Black Friday and holiday sales campaigns.


Evaluating Material Quality and Eco-Compliance Challenges


Beyond aesthetic consistency, modern supply chains face intense pressure regarding material integrity and environmental regulations. Sourcing colored mailers means balancing durability with sustainability demands, a dual requirement that many small-scale suppliers cannot fully satisfy.


Weak film structures, poor tear resistance, and faulty adhesive seals are frequent pain points when dealing with sub-par suppliers. Colored plastic films require precise formula adjustment to maintain both color purity and physical toughness. A compromised mailer risks damage during transit, leading to higher return rates. Extra forward‑thinking enterprises seek verified manufacturing standards, including strict in‑house quality control protocols and international certifications such as ISO compliance. Together, these measures deliver stable and standardized product performance in mass production.


Furthermore, regulatory shifts regarding sustainable packaging present both an opportunity and a risk. Markets across the globe are tightening regulations on single-use plastics. Many countries have launched strict packaging inspection policies to restrict non-recyclable and non-degradable plastic products. Brands sourcing pastel shipping solutions must verify whether their partners offer certified sustainable alternatives. For instance, reputable suppliers often provide eco-conscious pathways such as Global Recycled Standard (GRS) materials, encompassing pre-consumer and post-consumer recycled options, alongside fully biodegradable materials that are heavily favored in eco-conscious regions like Australia. These compliant eco-materials allow e-commerce brands to achieve green transformation while retaining their customized aesthetic packaging design.


Strategic Solutions Through Direct Source Partnerships


Mitigating these multi-layered procurement risks requires a shift away from complex distribution networks toward integrated suppliers. Direct manufacturing partners eliminate unnecessary middlemen, offering greater transparency and accountability from raw material procurement to final delivery. Every production link is traceable, allowing brands to solve quality and delivery problems efficiently once issues occur.


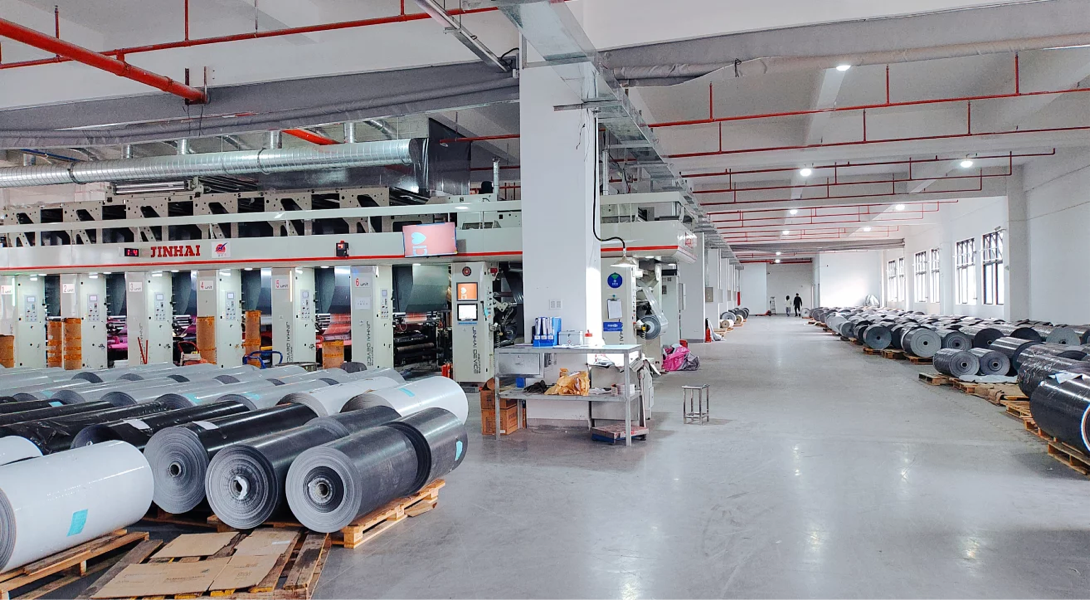
An industry specialist with deep manufacturing roots can better manage pigment consistency, stringent quality testing, and material innovation. For example, WH Packing leverages over fifteen years of manufacturing expertise as a dedicated B2B suppliers. By managing the entire production lifecycle in-house—ranging from raw material sourcing to extrusion and conversion—they help brands overcome standard supply chain friction. The team adopts standardized color calibration processes for customized pastel packaging, ensuring zero obvious color difference between different production batches.


Their extensive product portfolio includes specialized options such as light pink poly mailers, engineered to provide vibrant aesthetics without sacrificing film strength or durability. Alongside customized colored selections, they accommodate diverse enterprise needs through flexible customization parameters, robust cost-control measures, and reliable fulfillment timelines, perfectly matching the bulk procurement demands of medium and large e-commerce enterprises.


Securing Long-Term Resiliency in Packaging Logistics


Mitigating supply chain risks ultimately depends on proactive vendor selection and strategic alignment. As consumer expectations evolve, the demand for eye-catching and responsible shipping supplies will only intensify. B2B procurement professionals can safeguard their operations by prioritizing direct source manufacturers who combine rigorous quality assurance with versatile, eco-friendly material offerings. By establishing resilient partnerships early on, brands can navigate market fluctuations smoothly and keep their fulfillment operations running without interruption, building a stable and professional brand image in the competitive global e-commerce market.

October 12, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

Why All-in-One Smart Boards Are Becoming Popular in Modern Classrooms and Meeting Rooms

by apbclothing September 30, 2026
written by apbclothing

Modern classrooms and meeting rooms rely on more digital content than before. Teachers share lesson materials, teams present reports, and participants often need to write and display information in the same session. Traditional setups may require several separate devices and connection tools. An all-in-one smart board brings several of these tasks onto one interactive screen, making the room easier to use.


For K12 schools and small to medium-sized businesses, the Nework smart board is designed around intelligent display and collaboration needs. The brand has more than 20 years of professional audiovisual experience and focuses on touch interaction, wireless sharing, collaborative annotation, and smart management. They invite school purchasing teams and business buyers to discuss classroom or meeting requirements, including deployment, daily use, maintenance, and service needs, before selecting a solution.


Fewer Devices Can Make the Room Easier to Manage

A conventional room may depend on several separate devices. Users may need to connect a laptop, switch input sources, find the correct cable, and use another surface for writing. Each extra step can interrupt a lesson or meeting.


An all-in-one board reduces this equipment chain. Touch interaction, content display, annotation, and wireless screen sharing can be handled through one main device. This does not remove every supporting device, but it can reduce the number of items users operate during routine sessions.


For purchasing teams, fewer components can also simplify planning. They can compare one integrated setup with a room built from several products. This makes installation, training, and future maintenance easier to review.


Classroom Efficiency Depends on Simple Interaction

In a K12 classroom, technology should not take attention away from teaching. Teachers often move between explanation, visual materials, student questions, and board work within a short period. If changing tasks requires several devices, the class can lose useful teaching time.


Interactive boards make these transitions more direct. A teacher can display lesson content, write on the screen, add notes, and return to earlier material without moving between separate tools. Wireless screen sharing can also make it easier to present content from another compatible device.


Collaborative annotation is useful when teachers want students to discuss a diagram, sentence, calculation, or image together. The value is not simply that the board is digital. The practical benefit comes from reducing the steps between showing information and interacting with it.


Meeting Rooms Need Faster Starts and Clearer Collaboration

Small and medium-sized businesses often have meeting rooms used by different teams. Sales staff may present proposals, managers may review reports, and project groups may discuss schedules or designs. Complicated room controls can create delays when users are unfamiliar with the equipment.


An integrated smart board can shorten setup because key collaboration functions are placed on one interface. Teams can display material, annotate visible content, and share ideas without depending on a separate whiteboard for each discussion. That can help meetings move from presentation to discussion.


Wireless casting is another practical feature for shared rooms. It can reduce physical connection changes when participants need to show content from different devices. Buyers should still review compatibility with the devices and software already used by the organization before choosing a setup.


Lower Equipment Complexity Can Affect Total Cost

Purchase price is only one part of room cost. Schools and businesses also need to consider installation, accessories, staff training, maintenance, replacement parts, and time spent solving connection problems. A lower-priced collection of separate devices may not always produce lower operating costs.


An all-in-one design can simplify this calculation. When several daily functions are combined, purchasing teams may need fewer accessories and device types to manage. Standardizing similar rooms can also make staff training more consistent because users face a familiar operating method.


For schools with multiple classrooms or businesses with several meeting spaces, procurement teams can compare the complete room cost rather than only the screen price. Installation, expected use, management, and service arrangements should be included.


Deployment and Maintenance Matter After Installation

Technology is useful only when users can operate it with limited disruption. A school may have many teachers sharing equipment, while a small business may not have dedicated IT staff available in every meeting. Simple deployment and clear device management can therefore influence purchasing decisions.


Smart management functions can help organizations organize device use and routine administration. Requirements differ by site, so buyers should ask how devices are configured, updated, monitored, and maintained. They should also ask how technical assistance is handled.


For this reason, buyers evaluating a Nework smart board should look beyond touch and display functions. They can ask the brand about deployment procedures, maintenance needs, after-sales arrangements, and how the solution fits existing classroom or meeting workflows. These questions connect product features with long-term use.


What Buyers Should Compare Before Making a Decision

The growing interest in all-in-one smart boards comes from practical room needs. Schools want smoother teaching interaction, while businesses want meetings to start quickly and move between presentation and discussion with fewer interruptions. Both groups also care about cost, deployment, maintenance, and service over time.


A useful buying process should begin with the room itself. Buyers can review who will use the board, what content they need to share, how often the space is used, and which existing devices must remain compatible. These points make it easier to judge whether an integrated smart board fits the room.

September 30, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

How to Evaluate Hybrid Inverter Manufacturers?

by apbclothing September 11, 2026
written by apbclothing

When selecting a reliable production partner for clean energy infrastructure, the key is a rigorous assessment of technical credentials and engineering histories. Deploying a high-quality hybrid inverter solar framework serves as the foundation for modern residential and commercial microgrids. Partnering with sub-standard fabricators can lead to premature hardware breakdowns, firmware synchronization issues, or expensive system downtime. Evaluating precise operational benchmarks enables project planners to distinguish between short-term hardware assembly and long-term technological reliability.


Analyzing Manufacturing Quality and Compliance Standards

Industrial evaluation begins by auditing a supplier’s factory quality control systems and global safety certifications. Premium conversion equipment must pass rigorous thermal stress tests, high-voltage insulation tracking, and environmental sealing validations before leaving the assembly line. Certified tests verify internal switches can operate for decades under temperature changes. No sudden structural or performance failure should occur. A trustworthy hybrid inverter solar manufacturer prioritizes certified quality at every stage.


Evaluating Phase Flexibility and Load Balancing Technology

Advanced engineering capabilities are clearly demonstrated by how well a system manages uneven electrical distributions across multi-phase setups. Modern three-phase projects demand flexible circuit routing because real-time power consumption rarely remains perfectly uniform across all lines. Selecting hardware that features 100% unbalanced load support for diverse three-phase applications prevents internal voltage drops, safeguarding sensitive commercial machinery against phase instabilities and optimizing daily power utilization. The best hybrid inverter solar solutions excel in phase flexibility and load balancing.


Assessing Ecosystem Integration and Long-Term Field Reliability

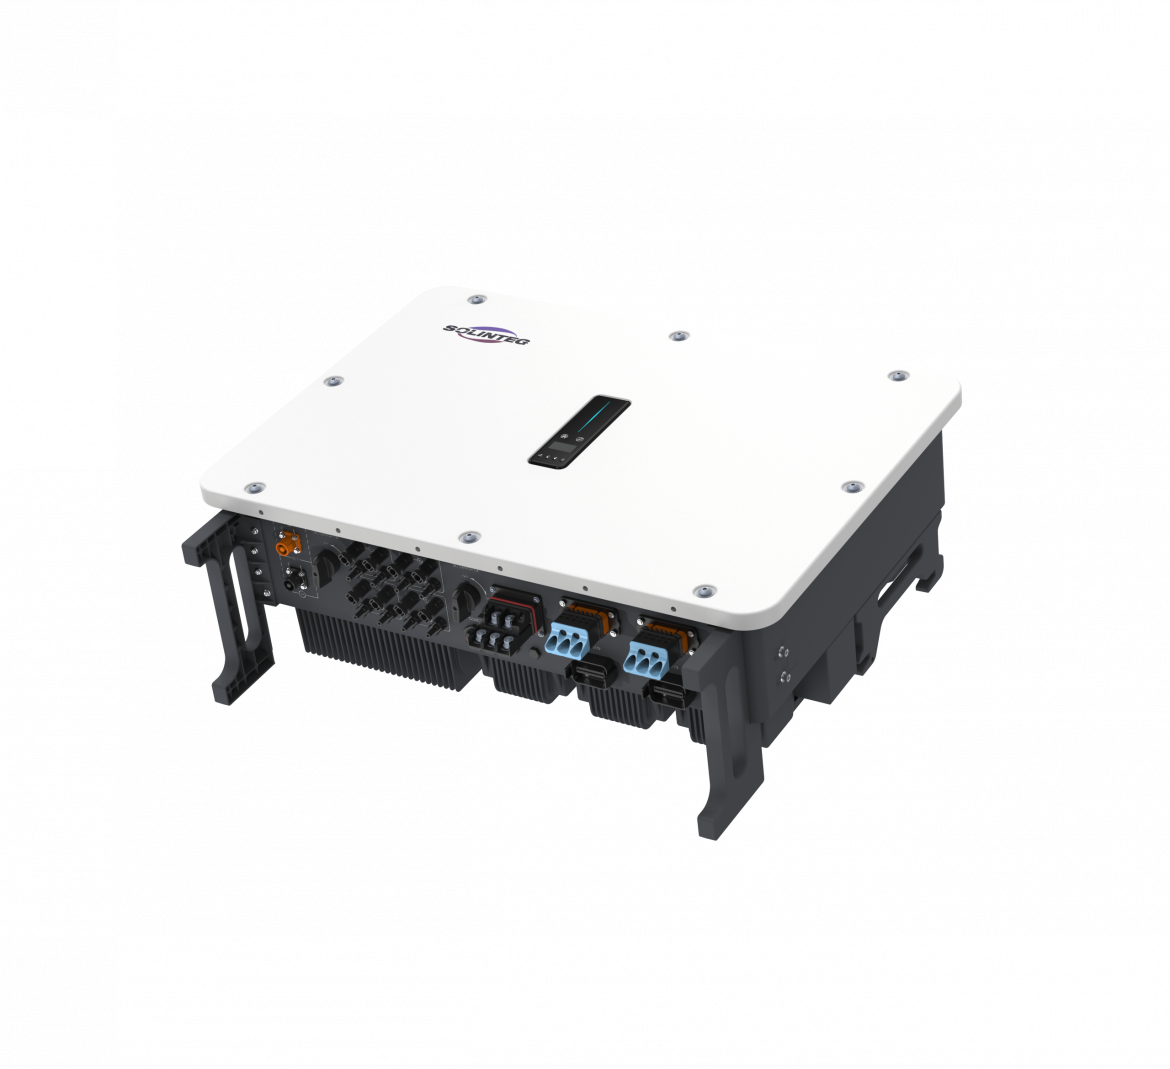
A resilient energy layout depends heavily on how smoothly conversion hardware interacts with battery blocks and monitoring software. Advanced system architectures developed by SOLINTEG focus on building open, cooperative ecosystems that reduce component communication lag. This focus on seamless digital integration lowers setup errors while maximizing raw current throughput. Choosing SOLINTEG units ensures that automated power routing remains stable through variable grid conditions without requiring constant manual maintenance.


Conclusion

Securing an optimal hardware supplier requires looking past simple wattage metrics to focus on phase flexibility and structural testing. Prioritizing comprehensive protection protocols and balanced phase architecture prevents unexpected failures when electrical loads shift unpredictably. Investing in factory-synchronized conversion units reduces installation complexities and optimizes daily solar harvesting ratios. Ultimately, choosing verified manufacturing excellence guarantees a highly resilient energy network that safely delivers independent power for decades.

September 11, 2026 0 comments
0 FacebookTwitterPinterestEmail
Machine

Methodologies for Verifying Industrial Hydraulic Press Machine Performance

by apbclothing July 23, 2026
written by apbclothing

Evaluating the operational output of manufacturing hardware is critical for maintaining high part quality. Industrial manufacturing facilities rely on precise metric tracking to verify that their equipment performs efficiently under continuous, heavy-duty production schedules.

System performance directly influences compound curing times, dimensional accuracy, and final part consistency. Analyzing physical key indicators helps engineering teams detect mechanical degradation early. This preventive approach avoids expensive component failures and protects corporate capital investments.

Evaluating Structural Integrity and Platen Alignment

The foundational step in performance verification involves measuring the structural rigidity of the press frame. Under heavy clamping loads, a low-quality frame will flex, causing uneven pressure distribution across the mold surfaces.

Engineers check platen parallelism using high-precision digital dial indicators at multiple points. Maintaining zero structural deviation is absolutely vital when molding low-durometer compounds. This stability prevents material leakage and ensures uniform parting lines.

Choosing a premium rubber injection molding machine manufacturer guarantees robust structural engineering. Top-tier machinery utilizes thick, stress-relieved steel plates designed to withstand intense hydraulic pressures. This rigid construction prevents structural deflection during demanding production runs.

Analyzing Hydraulic Pressure Stability and Response Time

Hydraulic architecture dictates how effectively a machine can execute complex clamping and injection sequences. Performance testing requires real-time monitoring of pressure fluctuations within the main hydraulic circuits during operation.

Advanced diagnostic tools track how quickly the system reaches its target clamping force. Severe pressure drops or slow response times indicate internal valve wear or pump inefficiencies. These issues can compromise the vulcanization process.

Partnering with an experienced rubber injection molding manufacturer ensures access to high-grade hydraulic systems. Premium machinery integrates specialized Rexroth valves and dual-pump architectures to stabilize fluid dynamics. This engineering ensures excellent repeatability across every cycle.

Verifying Thermal Uniformity Across Heating Platens

Precise temperature control is a non-negotiable factor when processing complex elastomeric compounds. Thermal validation involves mapping the platen surface using digital thermocouples to locate localized cold spots.

If temperature metrics fluctuate across the mold area, raw rubber compounds will cure unevenly. This imbalance causes structural air voids or surface blisters. These defects often lead to part failures during field testing.

An optimized vertical press built by HWAYI incorporates advanced PID temperature calibration software. This intelligent control system keeps platen temperature tolerances exceptionally tight. German-imported insulation plates further minimize heat dissipation into the frame. Only a professional rubber injection molding machine manufacturer can deliver precisely calibrated heating systems to support consistent rubber molding quality.

Measuring Injection Accuracy and FIFO Volumetric Precision

For injection-capable machinery, procurement teams must verify the volumetric accuracy of the injection unit. Testing involves running multiple material cycles and weighing the injected compound to check consistency.

Significant weight variations indicate poor screw metering or check-valve leakage inside the barrel. These flow fluctuations disrupt automated lines and increase scrap rates. Consistent volumetric output is crucial for high-tier industrial contracts.

Advanced platforms developed by HWAYI utilize First-In, First-Out (FIFO) injection architectures to optimize flow dynamics. This specific design ensures that the oldest material is injected first, eliminating material stagnation. This architecture delivers high injection accuracy.

Testing Degassing Efficiency and Auxiliary Automation

During the curing cycle, chemical reactions within rubber compounds release trapped air and volatile gases. Therefore, testing the efficiency of automated degassing, or “bumping” sequences, is critical for part validation.

The press control system must execute these micro-opening movements quickly and smoothly without dropping primary clamping forces too early. Poor degassing calibration causes severe cosmetic defects and weakens structural joint integrity.

Furthermore, auxiliary components like hydraulic core-pulling valves, ejectors, and sliding tables must operate seamlessly. Testing these automated mechanisms ensures the factory floor can run complex molds safely. This verification helps shorten total production cycles.

Monitoring Control System Repeatability and Data Logging

Modern industrial operations rely heavily on data integration to sustain high quality control standards. Performance validation must evaluate the responsiveness of the main programmable logic controller (PLC) network.

The control software must monitor critical variables in real time, including injection velocity, pressure curves, and thermal profiles. This continuous monitoring allows operators to detect subtle process shifts before defects occur.

Premium equipment setups feature integrated Siemens PLC systems that support comprehensive digital data logging. This technical capability provides the traceability required for strict automotive and aerospace manufacturing contracts. It also simplifies multi-station factory deployment.

Assessing Energy Efficiency and Long-Term Procurement Value

Evaluating total energy consumption during continuous operation is essential for calculating overall equipment effectiveness. High thermal dissipation or inefficient hydraulic loops cause massive utility overhead costs over time.

Engineering teams measure electrical draw during clamping, injection, and extended curing phases to assess efficiency. Modern energy-saving servo motors drastically reduce power usage compared to older, traditional constant-delivery pump systems.

High-performance molding equipment secures manufacturers’ long-term supply chains. CE-compliant machines can help meet relevant European safety requirements for applicable markets. Partnering with a certified rubber injection molding manufacturer delivers stable machine performance and consistent production compliance.

July 23, 2026 0 comments
0 FacebookTwitterPinterestEmail
MachineNewsTech

 Future Trends in High-Power EV Charging: Scaling with 40kW Modules

by apbclothing June 4, 2026
written by apbclothing

As the electric vehicle (EV) market continues to expand, the demand for high-power charging solutions is becoming increasingly critical. The introduction of the 40kW charger module is a significant development in this landscape, allowing for faster and more efficient charging at various locations. AcePower is a leading innovator in this field, showcasing how the 40kW EV charger module can support the evolving needs of the charging infrastructure.

Enhanced Durability and Efficiency of the 40kW EV Charger Module

AcePower’s 40kW charger module features a robust design that incorporates a full glue filling protection process. This innovation effectively isolates internal components from air, moisture, and dust, which not only extends the service life of the unit but also improves heat dissipation efficiency and structural stability. In a market where reliability is paramount, the durability offered by the 40kW EV charger module positions it as an ideal choice for demanding environments.

Additionally, the 40kW charger module is equipped with forced air cooling, allowing it to operate across an ultra-wide temperature range of -40℃ to +75℃. This capability ensures stable performance even under extreme climatic conditions, reducing the likelihood of performance degradation due to temperature fluctuations. Such advanced features are crucial for installations in varied locations, from urban charging hubs to remote service areas.

Meeting the Demands of the Modern Charging Landscape

As EV adoption rises, the requirements for charging infrastructure are evolving. The scalability offered by the 40kW EV charger module enables stations to handle higher volumes of vehicles efficiently. By delivering significant power in a compact form, this technology meets the needs of both public and private charging networks.

Moreover, the adaptability of the 40kW charger module enhances its appeal. It can accommodate diverse EV platforms and charging scenarios, ensuring that operators can offer versatile solutions. This adaptability is essential for attracting a wide range of customers in an increasingly competitive market.

Paving the Way for High-Power Charging Solutions

The future of high-power EV charging is closely tied to advancements in technology, particularly through the implementation of the 40kW charger module. With AcePower leading the way in innovation, operators can provide efficient and resilient charging solutions that meet the demands of the evolving electric mobility landscape. Embracing these advancements will be vital for ensuring the continued growth and sustainability of EV charging infrastructure worldwide.

June 4, 2026 0 comments
0 FacebookTwitterPinterestEmail
MachineManufacturer

Commercial cleaning robots for tobacco manufacturing: how to handle tobacco dust, loose packaging, and edge debris

by apbclothing May 22, 2026
written by apbclothing

Practical guidance for tobacco plant operations, EHS, facilities, and procurement teams evaluating dry sweeping robots in cutting, packaging, warehouse, wall-edge, pillar-edge, and equipment-edge zones.

2026-05-20 | 12 min read

In a tobacco plant, floor debris does not arrive in one tidy category. A cutting area can shed fine tobacco dust every few minutes. A packaging area can drop loose cigarettes, paperboard, cartons, film, labels, and broken packaging. A warehouse can add pallet chips, paper scraps, shrink-wrap, and general floor dust. The hard part is not finding a machine that can sweep. The hard part is deciding where robotic dry sweeping fits inside a cleaning program that also has combustible dust, worker exposure, traffic, production uptime, and narrow equipment clearances to consider.

The short answer: tobacco manufacturers should use commercial cleaning robots for repeatable floor-level dry debris, edge cleaning, spot cleaning, and high-frequency coverage in accessible areas. They should not treat a robot as the whole dust-control system. Combustible dust assessment, ventilation, dust collection, approved cleaning tools, manual touch-up work, and EHS procedures still define the safety envelope.

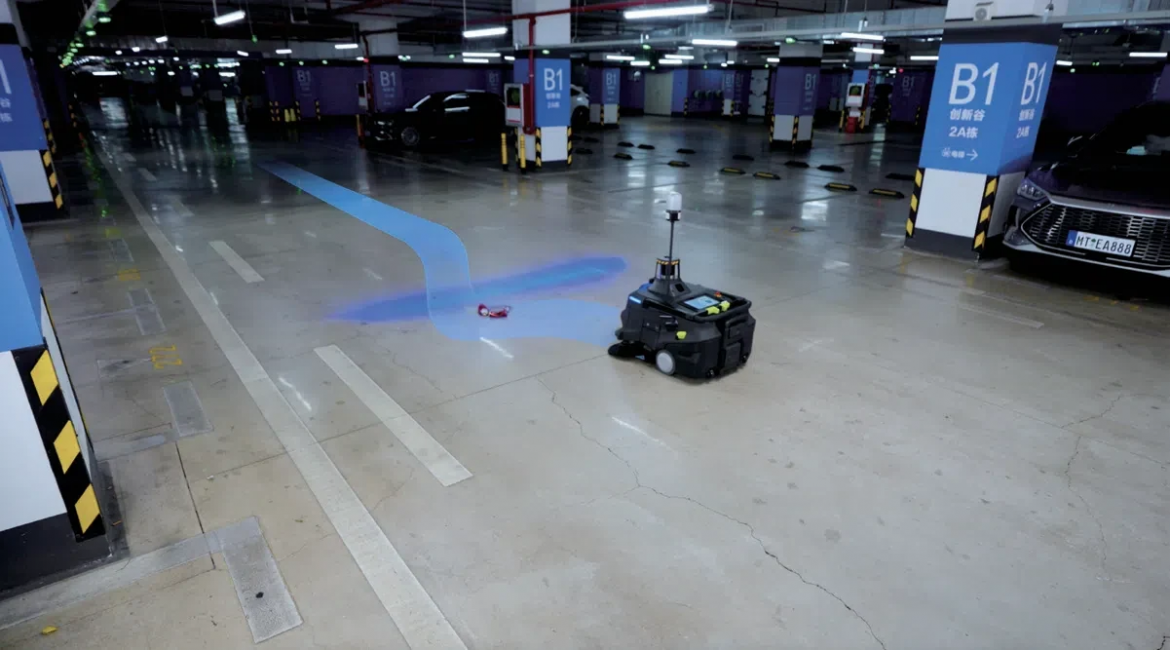
For large dry sweeping routes, PUDU MT1 Max is a relevant product to evaluate because it combines 3D perception, AI adaptive cleaning, 70 cm sweeping width, a 35 L waste container, edge-to-edge cleaning, automatic filter cleaning, IP54 sealing, and 5-10 hours of run time, according to Pudu Robotics. In tobacco manufacturing, the buying question is narrower: can the robot pick up the plant’s actual tobacco dust, scattered packaging, loose cigarettes, and edge debris while staying within the site’s EHS rules?

Why tobacco manufacturing is a difficult cleaning environment

Tobacco production creates a cleaning problem with three different behaviors.

First, fine tobacco dust spreads quickly. Cutting, conveying, blending, and transfer points can create settled dust on floors and equipment bases. If the cleaning method throws dust back into the air, the plant has not solved the problem. It has moved the problem into the breathing zone, onto overhead surfaces, or into nearby production areas.

Second, packaging debris is light but irregular. A sweeper may collect paper strips during one pass but push a flat carton edge, scatter plastic film, or miss a cigarette that lies close to a wall. Packaging zones need testing with real debris samples because the floor mix changes by line, material, humidity, and shift behavior.

Third, debris collects at edges. Wall bases, pillar bases, rack legs, guard rails, machine edges, dock doors, and blind corners are where tobacco dust and light scraps linger after central aisles look clean. Many factories overestimate automation coverage because they look at the open aisle first. The better test is the column base.

OSHA’s combustible dust material list includes “Tobacco blend” among agricultural dusts that can create combustible dust concerns when processed in powdered form. OSHA also points to regular housekeeping frequencies for floors and horizontal surfaces as part of dust control. That does not mean every tobacco floor has the same hazard classification. It means EHS should test and classify the facility’s dust and then define what cleaning equipment is allowed in each area.

Start with a zone-by-zone debris map

Before selecting a robot, map debris by production zone. A tobacco facility usually needs different settings, routes, and handoff rules for cutting, packaging, warehouse, and edge areas.

ZoneTypical debrisRobot fitHuman or EHS control still needed
Tobacco cutting and processingFine tobacco dust, small leaf fragments, settled dust near equipmentGood fit for frequent dry floor sweeping where the route is accessible and approved by EHSDust hazard assessment, dust collection, ventilation, approved cleaning method, filter maintenance
Cigarette packagingLoose cigarettes, paperboard, labels, films, carton pieces, paper scrapsGood fit after brush speed, suction or sweeping parameters, and spot-cleaning rules are tuned to the debris mixManual clearing below low equipment, under conveyors, and inside tight line-side gaps
Warehouse and stagingWood chips, pallet dust, paper scraps, shrink-wrap fragments, dust from trafficStrong fit for scheduled open-area routes and spot cleaning after staging activityForklift traffic rules, dock-area route limits, disposal routines
Walls, pillars, racks, and machine edgesDust lines, tobacco fragments, light scraps, corner buildupFit depends on edge-cleaning capability, route design, and safety-distance configurationManual detail cleaning in unreachable or safety-restricted areas

Table – Evaluation framework.

The purpose of this map is practical. It stops the team from asking “Can a robot clean our plant?” and moves the discussion toward “Which debris, in which zone, under which safety rules, at what frequency?”

Handle tobacco dust without simply spreading it

The most common legacy workflow in tobacco plants is also the one that deserves the most scrutiny: staff use compressed air to blow tobacco dust into a pile, then sweep the pile manually. In one anonymized U.S. tobacco manufacturing site, workers had to do this roughly every 20-30 minutes in a high-output cutting area. The labor burden was obvious, but the dust behavior mattered just as much.

OSHA describes combustible dust incidents through a simple set of conditions: fuel, oxygen, heat, confinement, and dispersion. Cleaning methods that disperse fine dust should be reviewed by EHS before they become routine. The safer direction is usually to collect settled dust more consistently, reduce dust migration, and prevent hidden buildup. That can involve source capture, dust collection, approved vacuums or sweepers, scheduled housekeeping, overhead inspections, and floor-level robotic cleaning where the equipment is allowed.

For robotic cleaning, the practical rules are:

– Use robots mainly for settled floor-level dust and small debris, not for airborne dust control.

– Confirm whether the robot and its electrical components are allowed in any classified or dust-hazard area.

– Define where compressed air is restricted, where vacuuming is required, and where robotic sweeping is acceptable.

– Inspect the robot’s waste container, brushes, and filters on a fixed schedule because tobacco dust can load a system faster than normal office or retail debris.

– Keep routes away from unstable dust piles that should be removed through site-approved procedures.

The buyer takeaway is simple: a robot can reduce repetitive floor sweeping, but dust safety has to be designed around the material, not around the machine.

Tune the robot for loose cigarettes and packaging waste

Packaging debris looks easy until the robot meets it at line speed. A loose cigarette can roll. A carton edge can catch. Thin film can float or fold. Paperboard can ride ahead of a brush if the robot approaches at the wrong angle.

This is where a generic cleaning demo often fails. The acceptance test should include tobacco-plant debris:

– Loose cigarettes in different orientations.

– Cigarette packs and flattened cartons.

– Paperboard tabs, labels, and small scraps.

– Plastic film and shrink-wrap fragments.

– Mixed piles of dust and light packaging waste.

– Warehouse debris such as wood chips and pallet dust.

PUDU MT1 Max is built for sweeping rather than wet scrubbing. Pudu Robotics states that MT1 Max can remove debris ranging from cigarette butts and paper scraps to large bottles, and its AI adaptive cleaning strategy can reduce power for light debris to limit scattering or increase power for heavier debris. For tobacco packaging areas, that is the right kind of capability to test because the concern is not only whether the robot sees debris. It is whether it collects the debris without pushing it into the next aisle.

The tuning process should be boring and strict. Choose a representative debris set, run repeated passes at different settings, count misses, inspect edges, then document which settings belong to each zone. If the robot cannot reach below a low conveyor or into a narrow service gap, mark that area for manual detail cleaning instead of forcing the route.

Edge debris is where acceptance tests should spend time

Open floors are the easy part. Tobacco dust at a pillar base is the real test.

Edge debris matters because it is visible, persistent, and easy to miss in a coverage report. A robot may show strong square-meter coverage while leaving a dusty line along a wall, a packing-machine foot, or a column guard. For a production manager, those edges are often the difference between “the robot worked” and “staff still have to chase the same mess.”

Pudu Robotics lists “0 cm edge-to-edge cleaning” for MT1 Max. In field terms, that capability should be translated into a route and test method:

– Run the robot along straight walls, pillars, columns, and machine bases.

– Test convex corners and concave corners separately.

– Check whether loose tobacco fragments at the base of a column are collected or pushed.

– Measure how the robot behaves near guard rails and fixed obstacles.

– Confirm safety-distance settings with EHS and site operations.

In the anonymized U.S. tobacco plant mentioned earlier, edge cleaning near pillars was one of the most important proof points. The site used a software configuration that allowed the robot to work very close to columns, helping it collect tobacco fragments around pillar bases. That field result should not be generalized blindly to every plant, but it gives procurement teams a useful test pattern: do not approve the robot only in the center aisle. Approve it at the edge.

Use robots where they reduce repetitive work, and keep manual cleaning where it belongs

Good automation in tobacco manufacturing is not a contest between workers and robots. The best deployments give routine, repeatable routes to the robot and keep judgment-heavy or unreachable tasks with trained staff.

Robots are a strong fit for:

– High-frequency sweeping in open cutting-area aisles.

– Packaging floors where loose cigarettes and packaging scraps fall repeatedly.

– Warehouse lanes, staging areas, and large dry floor routes.

– Spot cleaning when debris appears between scheduled routes.

– Edge routes along walls, pillars, and fixed equipment where the robot has been tested.

Manual cleaning remains necessary for:

– Under-equipment spaces the robot cannot enter.

– Complex narrow passages with frequent obstruction.

– Overhead dust, ledges, ducts, beams, and hidden horizontal surfaces.

– Any area where EHS requires a specific approved vacuum, tool, or shutdown procedure.

– Line-side cleanup that requires staff judgment during production.

This division of labor is what made the anonymized tobacco deployment credible. The customer understood that the robot could cover cutting, packaging, warehouse, and many edge-cleaning tasks, while staff would still handle machine bottoms and complex narrow spaces. That boundary is not a weakness. It is how a plant avoids overpromising automation and then losing trust after go-live.

A practical deployment pattern for tobacco plants

A workable tobacco-factory deployment usually follows four phases.

Phase 1: classify the cleaning zones

Start with EHS, facilities, production, and maintenance in the same walkthrough. Identify dust-generating processes, ordinary floor debris, traffic routes, blocked areas, and prohibited zones. Confirm where dry sweeping is allowed, where vacuuming is required, and where equipment must meet specific hazard classification requirements.

Phase 2: run debris-fit tests

Use real tobacco dust, real packaging scraps, real loose cigarettes, and real warehouse debris. Test open aisles, edge routes, column bases, dock areas, and packaging-line perimeters. Record misses instead of relying on a visual impression.

Phase 3: tune routes and cleaning parameters

Adjust approach angle, brush or sweeping parameters, spot-cleaning behavior, route frequency, safety distance, and waste-container service intervals. The goal is not the prettiest map. The goal is fewer repeated manual interventions in the same places.

Phase 4: define the operating handoff

Decide who empties the waste container, who checks brushes and filters, who reviews cleaning reports, who handles exceptions, and who owns route changes when production equipment moves. Robots fail quietly when no one owns the daily handoff.

What to ask in an RFP or pilot test

The best RFP questions are specific to the mess. Tobacco plants should ask vendors to prove the following items on site.

Evaluation itemWhat to verifyWhy it matters
Dust compatibilityEHS approval for the zone, filter and waste-container service plan, dust control boundariesTobacco dust may create exposure and combustible dust concerns
Mixed debris pickupLoose cigarettes, cartons, paperboard, film, labels, pallet chips, and dustPackaging floors rarely contain one debris type at a time
Edge cleaningWall bases, pillar bases, machine feet, guard rails, and dock thresholdsEdge debris drives manual touch-up workload
Navigation and trafficForklifts, pedestrians, narrow aisles, high ceilings, low light, reflective surfacesTobacco plants are dynamic production environments
Maintenance routineBrush checks, bin emptying, filter cleaning, software updates, fault handlingDust-heavy sites can load cleaning hardware quickly
ReportingCleaning area, route completion, missed-task notes, fault recordsFacilities teams need evidence, not just a completed route icon
BoundariesUnder-equipment gaps, complex narrow passages, classified areas, overhead dustClear limits prevent disappointment after deployment

Table – Evaluation framework.

If a vendor cannot run this test with the plant’s real debris, the evaluation is incomplete. If a vendor claims the robot can handle every cleaning job without manual follow-up, the claim should be challenged.

Where PUDU MT1 Max fits

PUDU MT1 Max is positioned by Pudu Robotics as an AI-powered 3D perception robotic sweeper for complex large-scale environments. Official specifications list VSLAM, marker navigation, and 3D LiDAR SLAM; a 70 cm cleaning width with side brush; a 35 L waste container; 5-10 hours of run time; charging time under 3.5 hours; 2200 sq m per hour maximum cover cleaning performance; and 7000 sq m per hour maximum spot-cleaning performance.

For tobacco manufacturing, the product relevance comes from five capabilities.

First, dry sweeping fits zones where water should be avoided. Many production areas do not want unnecessary wet cleaning near equipment, product material, or packaging lines.

Second, 3D perception can help in complex environments with pillars, traffic, high ceilings, and lighting interference. Pudu Robotics says MT1 Max uses 3D LiDAR plus multi-sensor fusion to map, detect obstacles, and navigate in demanding conditions.

Third, adaptive cleaning matters for light debris. If the robot uses too much force on paper scraps or tobacco fragments, it can scatter them. If it uses too little force on heavier waste, it can miss them. The site acceptance test should verify this balance.

Fourth, edge-to-edge cleaning fits the common tobacco-plant complaint that dust gathers at walls, columns, and equipment bases.

Fifth, automatic filter cleaning and a 35 L bin support longer routes, though the plant still needs a maintenance rhythm based on actual dust load.

The right procurement implication is not “buy one robot and the cleaning problem disappears.” The useful conclusion is more practical: if a tobacco manufacturer has large accessible dry-floor areas, repeated packaging debris, and visible edge buildup, MT1 Max belongs on the shortlist for an on-site debris-fit test.

FAQ

Can a commercial cleaning robot handle tobacco dust?

It can handle settled floor-level tobacco dust in accessible areas when the site permits robotic dry sweeping and the robot is tested against the actual dust load. It should not be treated as airborne dust control or combustible dust mitigation by itself. EHS should define the approved method for each zone.

Should tobacco factories use compressed air to blow dust into piles?

Compressed air can disperse fine dust, so it should be controlled by site procedure and reviewed by EHS. OSHA’s combustible dust guidance focuses on reducing dust accumulations and asks whether housekeeping removes dust from floors and other surfaces during operations. In many plants, more frequent collection of settled dust is a better direction than repeatedly moving dust through the air.

What debris should be included in a robot acceptance test?

Use tobacco dust, leaf fragments, loose cigarettes, cigarette packs, paperboard, plastic film, labels, shrink-wrap, wood chips, and ordinary warehouse dust. Place debris in open aisles, near walls, at column bases, beside machine feet, and around dock transitions.

Can a robot clean under production equipment?

Only where the robot physically fits, navigation is reliable, and EHS allows the route. Low equipment, complex narrow passages, and obstructed service areas should usually stay in the manual cleaning plan.

What matters most when evaluating edge cleaning?

Test the exact edge conditions that annoy the plant today: wall bases, pillar bases, equipment feet, rack legs, thresholds, and guard rails. Count leftover debris after multiple passes. A strong center-aisle result is not enough.

Conclusion: clean the workflow, not just the floor

Tobacco manufacturing needs a cleaning system that respects the material. Fine dust, loose packaging, and edge buildup each behave differently. A commercial cleaning robot can remove a large share of repetitive floor-level debris when the route is accessible, the safety rules are clear, and the debris-fit test is honest.

The next step is a controlled site evaluation: map zones, classify dust risks, test real debris, tune the route, document boundaries, and define the daily handoff. For plants where dust and packaging waste keep returning every few minutes, that kind of evaluation can turn robotic cleaning from an interesting demo into a practical operating tool.

May 22, 2026 0 comments
0 FacebookTwitterPinterestEmail
MachineManufacturer

Customizable Features of Modern BESS Containers

by apbclothing May 12, 2026
written by apbclothing

As the demand for efficient energy storage solutions increases, modern Battery Energy Storage Systems (BESS) have evolved to offer a range of customizable features that meet the diverse needs of businesses. These features are critical for ensuring that energy storage solutions can adapt to various applications—from renewable energy integration to industrial backup systems. This article will explore the customizable options available in BESS containers, highlighting the role of energy storage container manufacturers like Wenergy in delivering innovative solutions.

Modular Design and Scalable Capacity

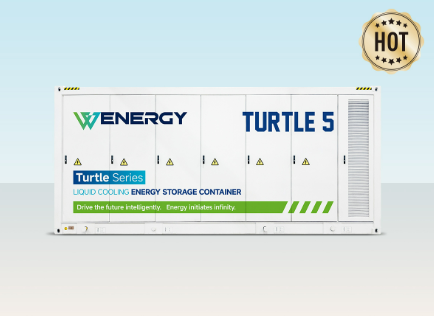
One of the standout features of contemporary BESS containers is their modular design, which allows for scalable capacity. Wenergy’s 5MWh Turtle Series Energy Storage Container exemplifies this adaptability, designed specifically for utility-scale applications. Each 20-foot container incorporates advanced liquid-cooled 314Ah battery cells, making it easy for businesses to expand their energy storage capacity as needed.

The modular approach not only facilitates scalability but also enhances operational efficiency. Businesses can start with a smaller installation and gradually increase their storage capabilities, thus aligning their energy resources with actual demand. This flexibility is particularly beneficial for energy storage container manufacturers, as it enables them to cater to the varying requirements of clients in different sectors, including renewable energy developers, utilities, and industrial operations.

Advanced Safety and Environmental Compliance

In addition to capacity scalability, modern BESS containers incorporate advanced safety features and environmental compliance measures. Wenergy ensures that their energy storage containers include intelligent thermal management systems and robust fire protection mechanisms. These features are critical for mitigating risks associated with battery storage, particularly in industrial and commercial applications.

Moreover, the design of the 5MWh ESS includes high corrosion resistance and compliance with global environmental standards, affirming its suitability for both urban and remote applications. These characteristics are vital for businesses concerned about sustainability and their environmental footprint. The advanced features also demonstrate Wenergy’s commitment to providing reliable and safe energy storage solutions.

The relevance of such safety features cannot be overstated, as many businesses are increasingly mandated to adhere to stringent safety and environmental regulations. By choosing an energy storage container manufacturer like Wenergy, companies can ensure that their BESS installations not only meet operational requirements but also comply with regulatory standards.

Enabling Custom Solutions for Diverse Applications

The customization capabilities of modern BESS containers empower businesses to tailor solutions for specific applications. Whether for renewable energy integration, industrial backup, or remote power generation, the ability to modify storage systems to meet unique needs is essential for operational success.

Wenergy’s BESS container factory focuses on delivering turnkey energy storage solutions that combine high-capacity battery modules with reliable power conversion systems (PCS). This integration is crucial for industries seeking seamless energy management. Additionally, the compact and fire-protected design of their containers allows for efficient deployment, minimizing the physical footprint while maximizing energy output.

As the energy landscape continues to evolve, the importance of customizable BESS containers becomes increasingly pronounced. These features not only enhance the viability of energy storage solutions but also enable businesses to operate more sustainably and effectively.

Advancing Energy Solutions for the Future

The customizable features of modern BESS containers play a pivotal role in addressing the diverse demands of the energy storage market. By focusing on modular design, advanced safety measures, and tailored applications, energy storage container manufacturers like Wenergy are paving the way for innovative energy solutions that cater to a variety of sectors.

In summary, the evolving landscape of BESS containers represents a significant advancement in energy storage technology. As businesses look for reliable, scalable, and adaptable energy solutions, the role of customizable features in these systems cannot be underestimated. By leveraging the expertise of a reputable energy storage container manufacturer, companies can secure future-ready solutions that meet their energy needs while promoting efficiency and sustainability.

May 12, 2026 0 comments
0 FacebookTwitterPinterestEmail
  • 1
  • 2

About Me

About Me

Hi there, my name is Ellen. Welcome to my Blog where you can get beauty tips and so much more.

Keep in touch

Facebook Twitter Instagram Pinterest Youtube Bloglovin

Recent Posts

  • Sodium Ion Batteries for Energy Storage vs Lithium-Ion: Key Differences Explained

    November 17, 2026
  • Maximizing ROI: Why Long Range RFID Antennas Are More Cost-Effective for Large Areas

    November 13, 2026
  • Real-Time UAV Fleet Monitoring: Improving Coordination, Positioning, and Mission Control

    November 10, 2026
  • How Machine Learning Algorithms Modernize Revenue Assurance in Telecom Operations

    November 10, 2026
  • Why Are Aerospace Companies Adopting a Handheld Laser 3D Scanner?

    November 10, 2026

Categories

  • Agriculture (1)
  • AR (1)
  • Beauty (21)
    • Hair Style (7)
    • Makeup (7)
    • Skincare (7)
  • Biology (3)
  • Business (86)
  • Catalyst (1)
  • Dentistry (1)
  • Desgin (2)
  • Dress (1)
  • Economy (25)
  • Featured (11)
  • Global Trade (30)
  • Healthcare (1)
  • Hotel (1)
  • Industry (139)
  • Innovation (56)
  • Jewelry (3)
  • Kitchen (2)
  • Knife (1)
  • LED (2)
  • Lifts (1)
  • light (1)
  • Living (1)
  • Machine (18)
  • Manufacturer (62)
  • Market (26)
  • Medical (13)
  • Monitors (1)
  • News (65)
  • Product (39)
  • Smart Lock (1)
  • Tech (75)
  • Technology (15)
  • Tool (5)
  • Vegetables indoor (1)
  • 未分类 (1)

About Me

About Me

Hi there, my name is Ellen. Welcome to my Blog where you can get beauty tips and so much more.

Popular Posts

  • 1

    Selecting the Ideal Fume Extraction System for CO₂ Laser Applications

    April 17, 2026
  • 2

    香港家庭首選的豪華MPV該具備哪些特點

    July 9, 2025
  • 3

    5 DIY Natural Skin Treatments For You

    January 22, 2019
  • 4

    Makeup Routine For A Dry Winter

    January 22, 2019

Featured Posts

  • Sodium Ion Batteries for Energy Storage vs Lithium-Ion: Key Differences Explained

    November 17, 2026
  • Maximizing ROI: Why Long Range RFID Antennas Are More Cost-Effective for Large Areas

    November 13, 2026
  • Real-Time UAV Fleet Monitoring: Improving Coordination, Positioning, and Mission Control

    November 10, 2026
  • How Machine Learning Algorithms Modernize Revenue Assurance in Telecom Operations

    November 10, 2026
  • Facebook
  • Twitter
  • Instagram
  • Pinterest
  • Youtube
  • Bloglovin

All Right Reserved. Designed and Developed by Apbclothing.


Back To Top
apbclothing
  • Home
  • Featured
  • Hair Style
  • Makeup
  • Skincare